Oct 29, 2026Guide
PVD Gold Colour Variation Between Batches: Why It Happens and How to Control It
Two PVD gold batches are never identical. What drives the colour shift, what tolerance is realistic, and the sampling process that keeps a multi-stage project consistent.
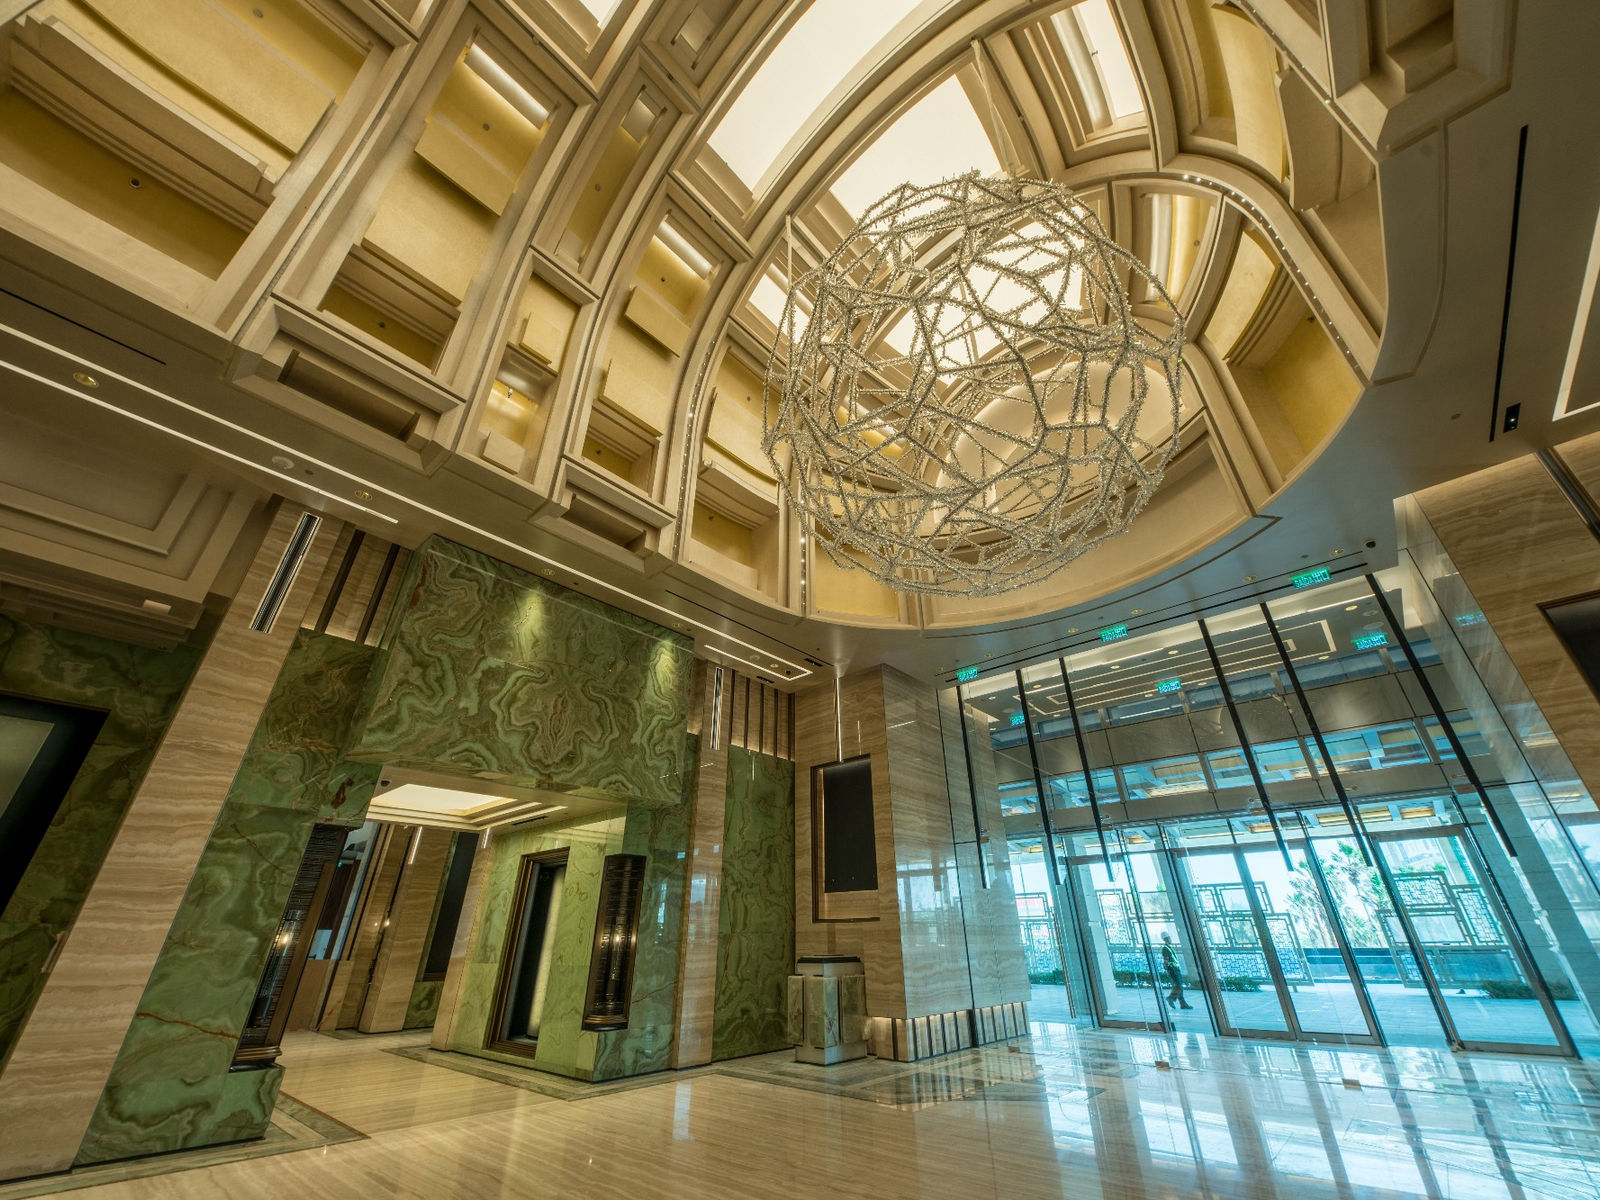
Every experienced specifier of PVD-coated stainless steel learns the same lesson eventually: two batches of "champagne gold" are never the same gold. The difference is usually small — visible mainly when two components sit side by side — but on a multi-stage project it becomes a defect claim if nobody planned for it. Understanding where the variation comes from makes it manageable.
Why PVD Colour Shifts
PVD (Physical Vapour Deposition, typically TiN or TiCN-based for gold tones) builds colour from a metal compound layer a few microns thick. The final tone depends on:
- Chamber conditions — gas ratio, temperature and target condition drift subtly between runs.
- Base material and finish — the same gold over a mirror-polished sheet reads different from over hairline or bead-blasted stainless, because the coating follows the substrate reflectivity.
- Layer thickness — a few tens of nanometres shift the tone measurably.
None of this means the process is out of control. It means colour is a range, not a fixed point — and the range must be agreed in advance.
What Tolerance Is Realistic
Within one chamber run, colour consistency is excellent — components processed together are effectively identical. Between runs, even from the same coater, a visible shift under direct side-by-side comparison is common and accepted in the trade when samples have been approved.
The realistic strategy is therefore not "zero variation" but "controlled grouping": components that sit next to each other get coated together; components on different elevations or floors can tolerate more.
The Sampling Process That Prevents Claims
- Approve a physical sample on the actual substrate and finish. Gold on hairline 304 is not gold on mirror 316. The sample must use the real material, thickness and polish.
- Split large orders into grouped batches by location. Give the coater a grouping plan: which components are adjacent in the finished space.
- Keep retained samples. Each approved batch keeps a control coupon, so later top-up orders match the project rather than the catalogue.
- Plan spares with the batch. Spare components coated in the same run cost little now and are unobtainable later.
Communicating It to the Client
The single sentence that saves disputes: "PVD colour is approved per physical sample and per batch grouping; minor variation between batches is inherent to the process." Put it in the submittal, attach the sample, and colour stops being a surprise.
Talk to the Coater Early
Champagne, rose gold, bronze and black each behave differently, and different coating plants have slightly different palettes. Bring your finisher in at design stage with your grouping plan — on hotel and casino projects this planning is routine, and it is the reason large PVD packages read as one continuous finish from lobby to lift.