Guide
Engineering Coordination for Complex Curved Brass Cladding
Curved brass cladding succeeds or fails in coordination, not fabrication. How shop drawings, 3D simulation and factory trials kept 3,000+ components on schedule.
Why curved brass cladding is a coordination problem, not a fabrication problem
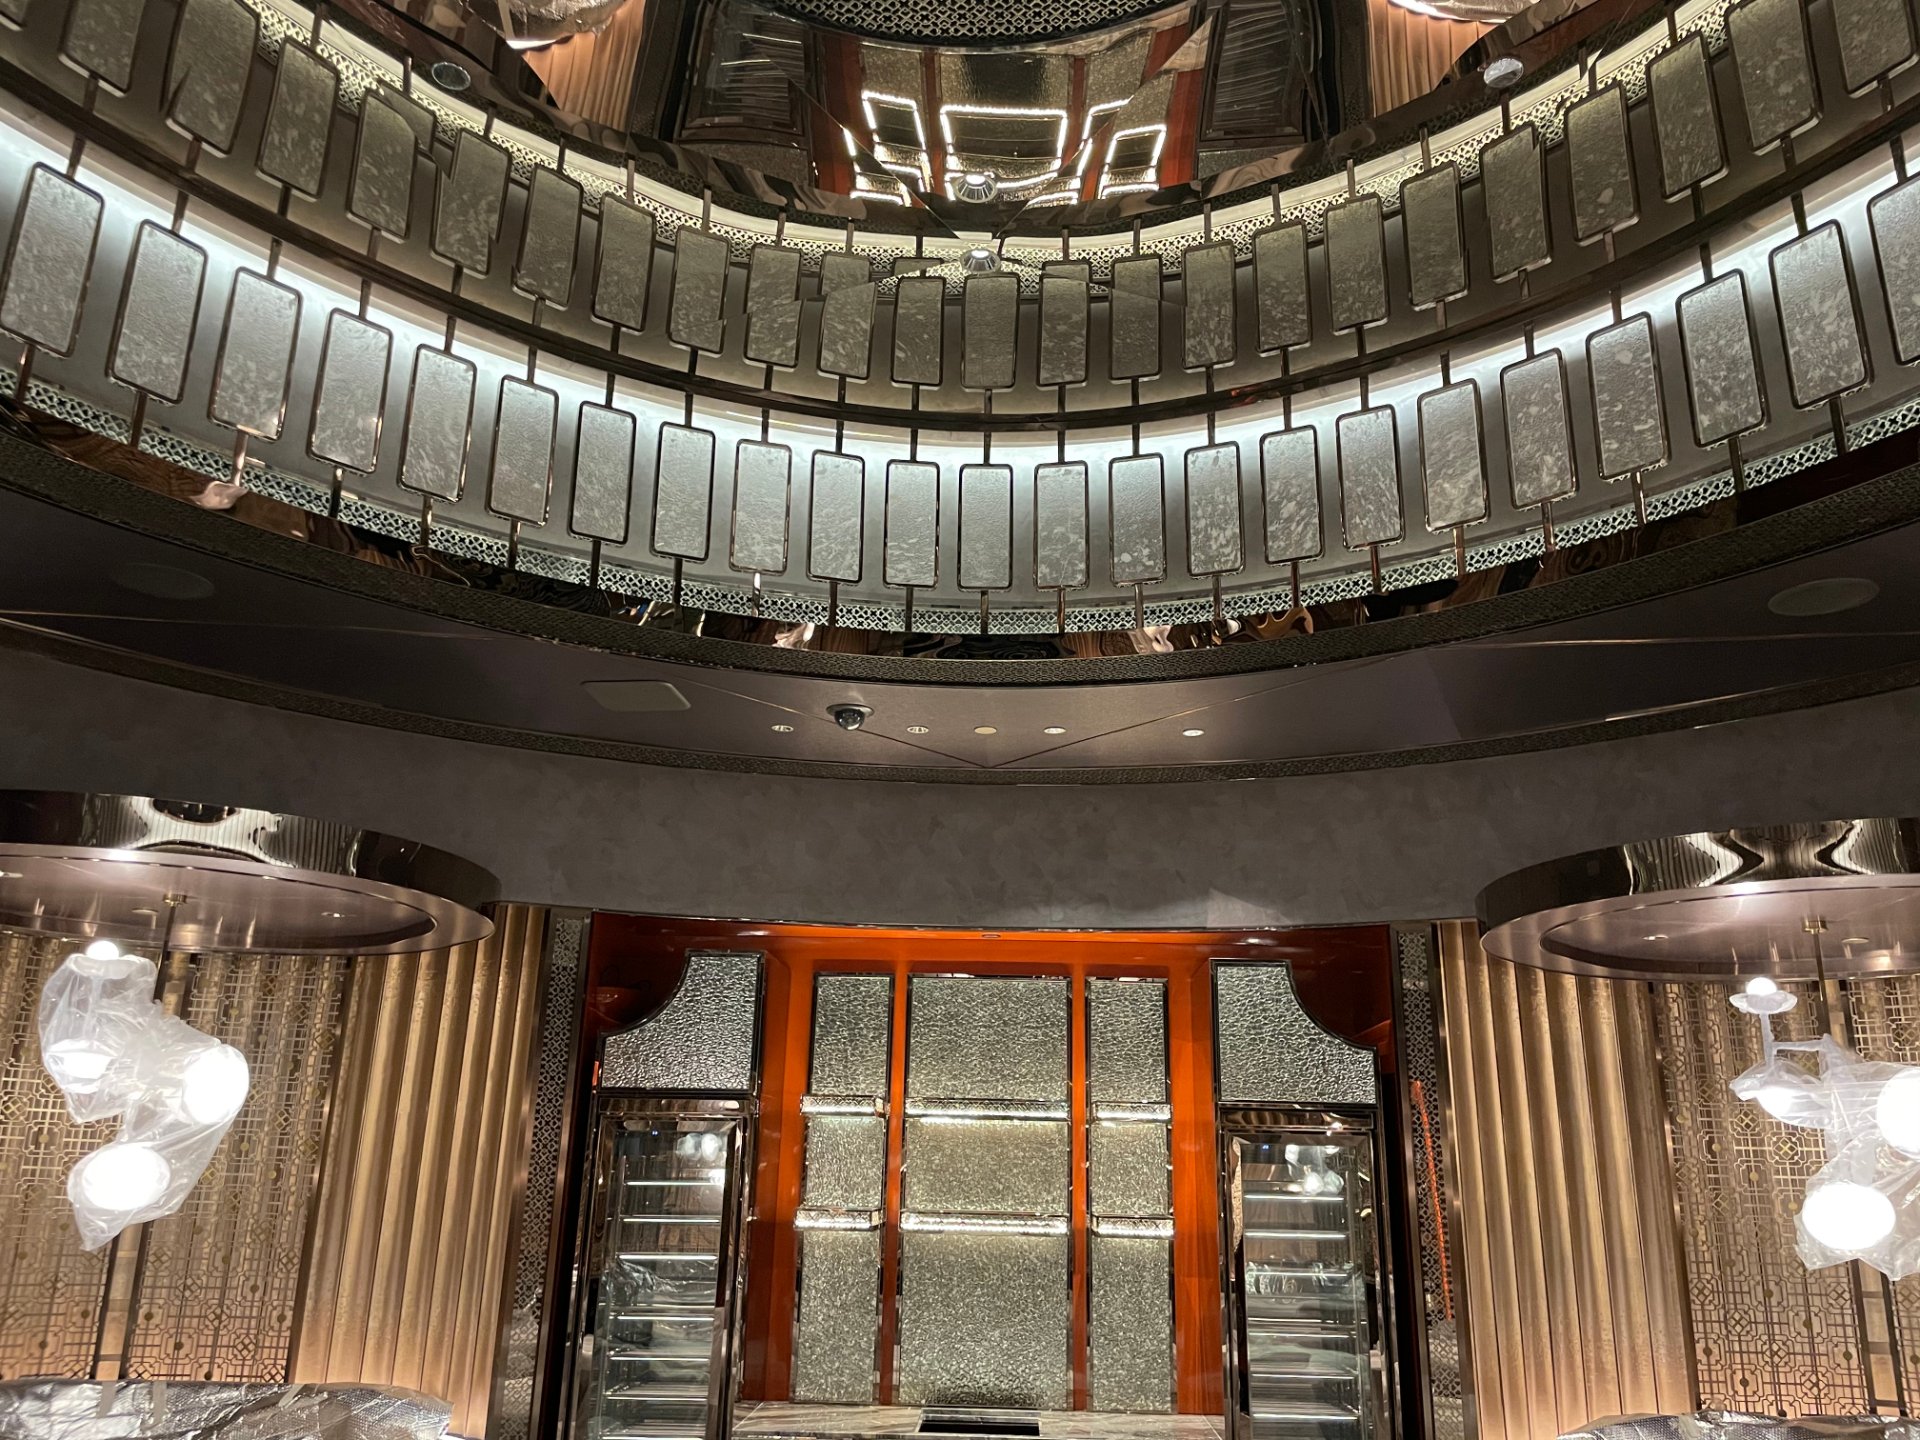
Curved brass surfaces photograph beautifully and age beautifully, which is why architects keep specifying them for lobbies, feature walls and column surrounds. What the rendered image does not show is the coordination load behind every curve: every segment must meet its neighbour within a visible tolerance, every opening must land on a structural datum, and every trade that penetrates the surface must be located before the first panel is cut.
On flat projects, a mis-measured panel is a local problem. On curved projects, a mis-measured panel is a systemic one, because the error propagates around the curve and shows up three segments away from where it was made. This article describes the coordination process we use on complex curved brass packages, illustrated with a 2,700 m² interior brass cladding package for the Australian War Memorial in Canberra, which involved more than 3,000 fabricated components and over 2,000 unique part codes.
Phase 1: Fix the reference geometry before anything is cut
The single most important coordination decision happens before fabrication: agreeing which model or drawing set governs the geometry. For curved work, a 2D elevation is not enough. The fabricator needs either the designer's 3D reference model, or a mutually agreed set of sections and control curves from which the panels can be developed.
Once the reference is fixed, shop drawings translate it into manufacturable segments. This is where most of the real engineering happens:
- Segment splits. Where the curve is divided into panels determines seam positions, panel size limits, polishing direction and how much cold or roll forming each piece needs. Splits that ignore material width or forming radius create panels that cannot be made flat-true.
- Tolerance stack-up. Each joint in a run of curved panels consumes part of the overall tolerance budget. Substructure tolerances, panel fabrication tolerances and installation tolerances add up across a curved run far faster than across a flat wall, so the drawing set must assign tolerance deliberately rather than leave it to the shop floor.
- Interfaces. Lighting coves, reveal joints, floor and ceiling abutments, and any penetration for services must be dimensioned to structural datums, not to nominal architectural dimensions.
On the War Memorial package, shop drawings went through structured review rounds with the project team, including video conference drawing reviews where curved segments were walked through line by line. Several revisions came out of these sessions, each cheaper to make on paper than on brass.
Phase 2: Simulate the installation before shipping anything
The second coordination instrument is a 3D installation simulation. Its purpose is not visualisation; it is interference detection and sequence planning.
When more than 3,000 components must arrive on site and install in a defined order, the questions a simulation answers are concrete: does this curved segment clear the adjacent trade's structure along its installation path, does the fixing zone of one panel collide with the substrate of another, and which components must be installed before which. On the War Memorial project, conflicts on curved segments were identified in the simulation phase and corrected before the components were fabricated and shipped. None of those conflicts would have been cheaper to resolve on site, where the remedy is usually rework: cutting, re-polishing, or remaking a finished brass panel.
For overseas projects the stakes are higher, because the correction loop crosses an ocean. A conflict discovered during simulation costs a drawing revision. The same conflict discovered during installation costs air freight, schedule and finish quality.
Phase 3: Code every part so the site never guesses
Curved packages generate a part count that manual tracking cannot carry. The War Memorial package used more than 2,000 unique part codes, managed with a five-point coding system that ties each physical component to its shop drawing, its position in the installation sequence and its carton.
Coding sounds like administration, but it is a coordination tool. It lets installation crews pick the right panel the first time, lets supervisors verify progress against the simulation sequence, and lets the factory prove that every code was manufactured, finished, inspected and packed. On a curved wall, where two adjacent panels may look nearly identical but install in only one orientation, unambiguous identification is what prevents a "near miss" fit from being forced.
Phase 4: Trial-fit in the factory, then pack in reverse order of installation
Factory pre-assembly is the final coordination checkpoint. Assembling representative runs of curved segments on the factory floor verifies joint alignment, reveal consistency and fixing positions while corrections are still cheap. For the War Memorial package, components were trial-fitted before dispatch, so the interfaces that the simulation predicted would work were physically proven.
After trial fit, packing is planned around the site sequence: components are packed so that the parts needed first come off the truck first, and finished surfaces are protected for the whole journey. For context on how large metalwork is packed for international shipments, see our article on packing large metalwork for overseas projects.
What your fabricator needs from you
Coordination is a two-way obligation. To run this process, the fabricator needs:
- The governing reference model or agreed control geometry, with a stated version.
- Structural datums and tolerance expectations for the substrate, from the main contractor.
- Interface information for adjacent trades: lighting, glazing, stone, joinery and services.
- A decision loop with authority — drawing reviews that produce answers, not more open questions.
In return, the deliverables you should expect are a segment split proposal, a tolerance allocation, a coded drawing set, installation simulation for complex zones, and evidence of factory trial fit.
The economic argument in one paragraph
Every one of these phases exists because the cost of correcting an error multiplies as the project advances. A conflict caught in drawing review costs a revision. Caught in simulation, it costs remodelling time. Caught at factory trial fit, it costs rework hours in the workshop. Caught on site, it costs finished brass, freight, programme and the installer's confidence in the whole package. The War Memorial package moved every solvable problem to the earliest possible phase, and that is the real reason a 3,000-component curved brass package can install smoothly on the other side of the world.
If you are evaluating a curved cladding package — brass, stainless steel, or a combination — send us your drawings for a technical review and quotation. We will tell you where the coordination risks are before you commit to a price.